Anodized 6000 Series Aluminium Profile Sections with Cutting Service Aluminum Frame Profile
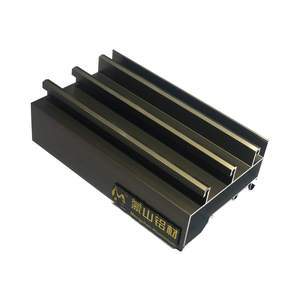
High-strength architectural framing sections delivered with precision burr-free high-speed circular saw cutting, micro-machined for modular equipment frames.
Precision Architectural & Industrial Alloy Sub-Assemblies Engineered for Chūkyō Industrial Region Fabricators
Compliant with JIS structural tolerances, micron-controlled anodic oxide film finishes, and modular CNC cutting operations tailored for Aichi Prefecture builders and system houses.
High-strength architectural framing sections delivered with precision burr-free high-speed circular saw cutting, micro-machined for modular equipment frames.
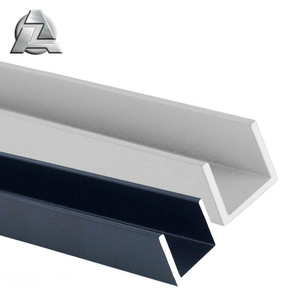
Structural track extrusions offering exact web-to-flange squareness, uniform alloy wall dimensions, and superior mechanical load bearing for linear sliding runs.
Architectural framing sections treated with sealed microporous anodic films resisting coastal humidity, environmental smog, and installation site scuffs.
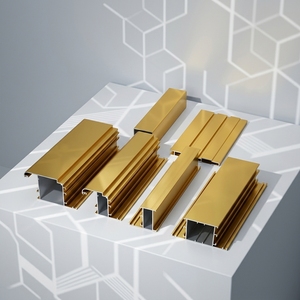
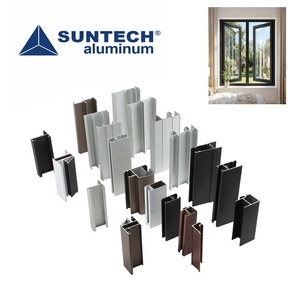
Precision multi-chamber profiles engineered for multi-tier thermal barrier strips, meeting both European structural stability and strict Japanese airtightness benchmarks.
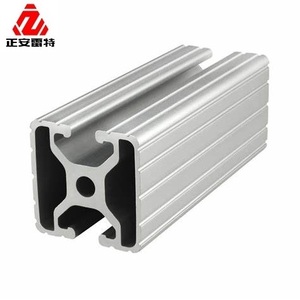
Engineered T-slot geometry accommodating universal JIS and ISO standardized fastener hardware, suited for cleanroom partition frames and production tooling.
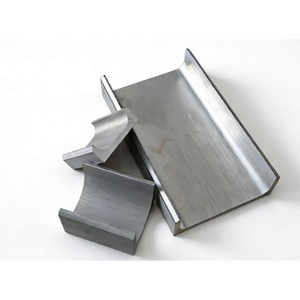
Metric-calibrated standard channel extrusions fabricated to sharp bend radii, uniform cross-sectional density, and impeccable electro-chemical clear anodizing.
High-rigidity alloy sections optimized for robotic machine enclosures, dynamic conveyor chassis, and industrial workstation frameworks throughout Toyota-City clusters.
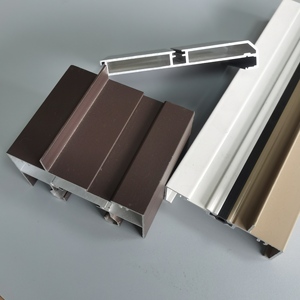
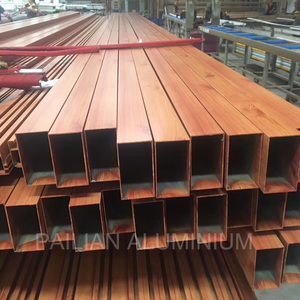
Sublimation-printed wood-grain coatings combining organic residential Japanese interior aesthetics with fire-retardant, rot-proof extruded aluminium structural cores.
The Chūkyō Industrial Area encompassing Aichi, Gifu, and Mie prefectures represents Japan’s premier precision manufacturing territory. From the automotive assembly lines in Toyota City to cutting-edge aerospace facilities in Kakamigahara and advanced architectural developments surrounding Nagoya Station (Meieki), the demand for standardized aluminium profiles goes far beyond standard off-the-shelf catalog shapes.
General commercial extrusions frequently fall short of the rigorous mechanical thresholds demanded by Japanese general contractors (Zenecon) and machine equipment builders. Issues such as profile twist, longitudinal camber, wall thickness deviation, and erratic anodic film oxidation cause substantial downtime in automated fabrication cells. Our manufacturing facility resolves these supply-chain bottlenecks through tightly monitored metallurgy, using primary A00 virgin ingots and tight billet homogenization.
By shipping directly from our extrusion and fabrication mills into the Port of Nagoya, Tier-1 and Tier-2 suppliers gain predictable delivery cycles, custom protective packaging to prevent sea-freight corrosion, and certified mill test reports (MTR) matching Japanese QA documentation.
Every extrusion batch intended for the Nagoya industrial and commercial sectors undergoes rigorous spectrometer chemical verification, eddy-current film thickness inspection, web squareness testing, and automated optical profile scanning to eliminate dimensional variance before dispatch.
How our standard aluminium profiles, custom structural channels, and advanced surface finishes integrate into local mechanical, architectural, and transport assemblies.
Toyota-City and Kariya factory floors rely heavily on modular 40x40, 45x45, and 60x60 industrial T-slot profiles for automated guided vehicle (AGV) chassis, robotic machine safeguarding, conveyor side guides, and lean workcell benches. Extrusions are optimized for rigid vibration resistance and universal t-nut hardware compatibility.
Nagoya's urban centers demand high seismic ductility and high-wind performance under typhoon loadings (exceeding 2400 Pa). Our hollow structural sections, thermally isolated window profiles, and heavy mullions act as the primary framing cores for commercial facades, high-rise luxury condominiums, and seismic retrofits.
Semiconductor sub-tier plants in Mie and distribution hubs along the Isewangan Expressway incorporate our high-micron anodized U-channels and rectangular tubes. Anodized oxide films (exceeding AA15 class) prevent microscopic particle shedding, creating durable hygienic perimeter partitions.
Compare mechanical properties, tempering regimens, and international standard cross-references for Nagoya fabrication orders.
| Alloy & Temper | Tensile Strength (Rm) | Yield Strength (Rp0.2) | JIS / EN Equivalence | Recommended Nagoya Application |
|---|---|---|---|---|
| 6063-T5 | ≥ 160 MPa | ≥ 110 MPa | JIS H4100 A6063S / EN AW-6063 | Architectural storefronts, slim sliding doors, decorative trims, curtain wall mullions. |
| 6063-T6 | ≥ 215 MPa | ≥ 170 MPa | JIS H4100 A6063S / EN AW-6063 | High wind-load building facades, high-bay louvers, structural exterior framing. |
| 6061-T6 | ≥ 260 MPa | ≥ 240 MPa | JIS H4100 A6061S / EN AW-6061 | Factory automation frames, heavy industrial tracks, AGV carriages, machining blocks. |
| 6005A-T6 | ≥ 270 MPa | ≥ 225 MPa | JIS H4100 A6005AS / EN AW-6005A | Heavy commercial decking, solar canopies, high-span industrial platform ladders. |
Key shifts influencing structural aluminium sourcing across Aichi, Gifu, and Mie prefectures over the coming decade.
With Japan mandating tighter energy-conservation standards for both commercial buildings (ZEB) and residential developments (ZEH), Nagoya developers are shifting away from plain profiles. Standard extrusions are now engineered specifically for polyamide thermal breaks, cutting thermal bridges and eliminating interior condensation during Chūbu winters.
Historically, Chūkyō manufacturing relied entirely on multi-tier domestic trading companies (shosha), which incurred notable markups and inflexible delivery schedules. Plant engineers and procurement officers are increasingly engaging direct-factory suppliers who can manufacture custom profiles to JIS dimensions while providing ocean shipping straight to Nagoya Port.
Facing skilled labor shortages throughout Japan's construction and industrial assembly sectors, buyers require factory-machined sections. Extrusions are pre-cut with tight angular accuracy (±0.5°), tapped, punched, and packaged as labelled kits that install directly on site without secondary trimming.
From metallurgical control to dedicated crating, our production network delivers accountable manufacturing at global export scale.
Operating a battery of high-capacity extrusion presses ranging from 600 tons up to 3,600 tons, our factories handle solid shapes, multi-cavity hollows, and large-web sections. In-house precision die production allows rapid prototyping and immediate turnaround on standard JIS-specified profiles.
Equipped with fully automated vertical electro-coloring and horizontal anodizing lines capable of clear, champagne, bronze, and deep black anodizing up to Class AA25. Powder coating capabilities utilize Qualicoat-certified fluorocarbon (PVDF) paints designed to resist UV degradation and chemical exposure.
Preventing transport damage is critical for Japanese jobsites. Every bundle is wrapped in non-scratch protective film, interlayered with pearl foam cushioning, capped with structural corner protectors, and securely packed in fumigated plywood cases tailored for containerized sea shipment to Nagoya Port.
Clear, definitive technical clarifications addressing standards, logistics, tolerances, and quality verification for the Nagoya market.
Yes. While European (EN 755/12020) and American (ASTM B221) standards are widely supported, all extrusions destined for Japanese fabricators are manufactured in compliance with JIS H4100 special precision class dimensions. We provide certified mill test sheets (Kensa Shomeisho) covering elemental chemical balance and tensile/yield yield performance per batch.
Ocean transit from our manufacturing hubs to the Port of Nagoya typically takes between 10 to 14 days, with customs handling and inland drayage across Aichi, Mie, and Gifu adding 3 to 5 business days. We coordinate complete export documentation including Bill of Lading, Certificate of Origin, and packing lists with designated Japanese clearing agents.
Yes. Our secondary processing facility operates 3-axis, 4-axis, and 5-axis CNC machining centers capable of handling profiles up to 6.5 meters long. We execute end miter cuts, thermal-break crimping, drainage weep slots, fastener counter-bores, and robotic tapping directly from your CAD/DXF data, reducing your local labor load.
For inland applications, JIS Class AA10 (film thickness ≥ 10 μm) is standard. For exterior facade profiles, coastal installations near Ise Bay, or chemical production environments, we specify JIS Class AA15 (15-20 μm) or AA20 (20-25 μm) sealed anodized coatings with high corrosion and weather resistance.
Profiles are protected with clean-peel PE surface protective film, bundled with heat-shrink wrapping, cushioned with composite pearl cotton between tiers, and sealed inside fumigated solid-timber or heavy plywood crates with desiccant packs to eliminate condensation corrosion during maritime voyages.
For standard catalog shapes (such as industrial U-channels, equal angles, and structural square tubes), MOQs start at 500 kg per section size. For custom custom-designed profile dies matching proprietary window systems or factory tooling, MOQs typically range from 1,000 kg to 3,000 kg, with die tooling costs rebated against scheduled volume targets.